OEE Metric: How to Measure
and Improve Equipment Effectiveness
Demystifying OEE, eliminating the Six Big Losses, and practical steps to drive overall equipment effectiveness on the shopfloor.
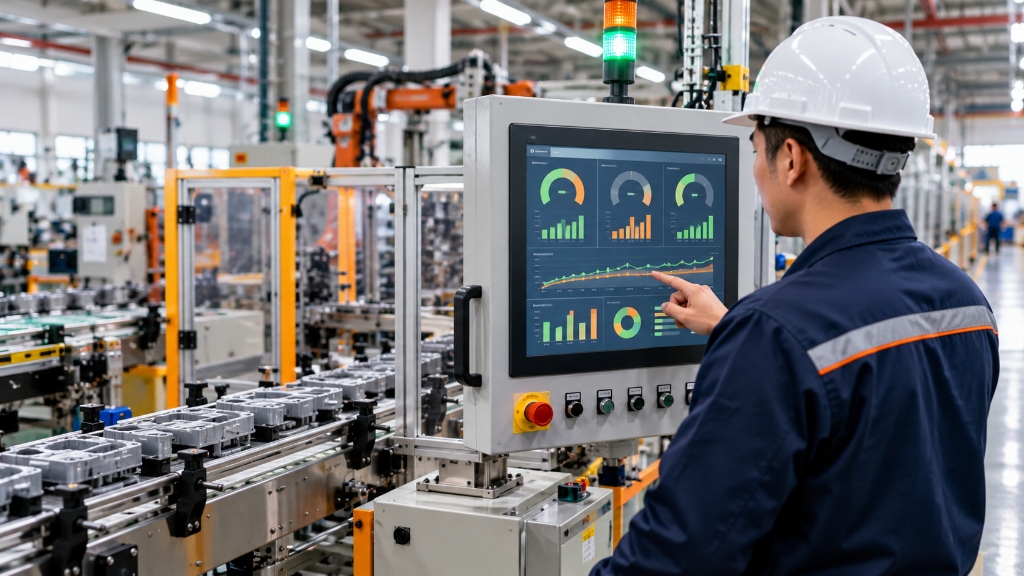
OEE (Overall Equipment Effectiveness) is a vital metric helping manufacturers quantify equipment utilization, uncover hidden losses, and implement targeted improvements. This guide walks you through calculating OEE, diagnosing the Six Big Losses, and executing a practical roadmap to elevate operational performance.
1. What is OEE?
— OEE (Overall Equipment Effectiveness) is the gold standard for measuring manufacturing productivity, reflecting the proportion of truly productive manufacturing time spent producing good parts at ideal cycle speed.
Is the machine truly operating during scheduled production hours?
When running, is the machine operating at maximum designed cycle speed?
How many units meet strict quality specifications on the first pass?
The proportion of planned manufacturing time truly productive at ideal cycle time without defects.
2. Calculating the Three OEE Factors
— OEE is calculated from three constituent factors: Availability, Performance, and Quality. Each metric reflects a critical dimension of the operational process.
- Example:
- •Planned Production Time: 450 minutes
- •Actual Operating Time: 405 minutes
- Example:
- •Ideal Cycle Time: 0.5 min/unit
- •Total Output: 700 units
- •Actual Operating Time: 405 minutes
- Example:
- •First-Pass Good Units: 680 units
- •Total Output: 700 units
3. Complete OEE Calculation Example
— Below is an illustrative calculation for an 8-hour production shift.
| Operational Parameter | Value | Notes |
|---|---|---|
| Total Shift Time | 450 minutes | 8 hours |
| Planned Non-Production Breaks | 30 minutes | Lunch, scheduled shift meetings |
| Planned Production Time | 450 minutes | Shift time minus planned downtime |
| Unplanned Downtime | 45 minutes | Breakdowns, die changeovers |
| Actual Operating Time | 405 minutes | |
| Ideal Cycle Time | 0.5 min/unit | |
| Total Output Produced | 700 units | |
| First-Pass Good Output | 680 units | |
| Defects / Rework | 20 units |
4. The Six Big Losses Affecting OEE
— OEE is driven down by the Six Big Losses, categorized under Availability, Performance, and Quality losses.
(Unplanned Stops)
Unplanned equipment breakdowns and mechanical or electrical failures.
(Changeover & Tuning)
Downtime during tooling changes, SKU changeovers, and warm-up adjustments.
(Idling & Minor Stoppages)
Brief stops (< 5 minutes) caused by part misfeeds, sensor blocks, or material starvation.
(Slow Cycles)
Equipment running below standard nameplate or ideal design capacity.
(Warm-up Scrap)
Off-spec parts generated during machine warmup and initial calibration.
(In-process Scrap & Rework)
Defective units and scrap produced during steady-state manufacturing.
5. Practical Roadmap to Improve OEE
— To sustainably boost OEE, plants need a structured roadmap integrating people, standard processes, and digital tools.
- •Collect accurate downtime & cycle data
- •Quantify the Six Big Losses
- •Isolate root causes with 5-Why & Pareto
- •Prioritize top downtime bottlenecks
- •Define SMART target KPIs
- •Build detailed countermeasure action plans
- •Implement TPM & autonomous maintenance
- •Standardize SOPs & SMED changeovers
- •Operator upskilling & engineering Kaizen
- •Track daily shift OEE performance
- •Audit compliance against plant benchmarks
- •Institutionalize standard work plant-wide
6. OEE Benchmark Levels & Interpretation
— OEE benchmarks vary across industries. The table below provides standard industry reference tiers to evaluate your plant's status.
| OEE Level | Benchmark Range | Operational Significance | Strategic Recommendation |
|---|---|---|---|
| Low | < 60% | Sub-optimal performance, severe hidden losses | Urgent need to diagnose root causes and tackle low-hanging fruit |
| Average | 60% – 75% | Standard operational level with significant upside potential | Deploy focused Lean & TPM initiatives to eliminate top downtime drivers |
| Good | 75% – 85% | Strong performance, highly stable shopfloor flow | Fine-tune micro-stoppages and institutionalize standardized maintenance |
| World-Class | > 85% | World-class excellence, industry-leading efficiency | Sustain operational discipline and scale best practices across all lines |
7. Key Takeaways & Recommended Next Steps
— OEE is a foundational yet powerful metric for uncovering hidden capacity and boosting throughput. Precise measurement, root-cause diagnosis, and disciplined Kaizen empower manufacturers to optimize unit costs and build operational agility.
- Start by measuring OEE on your primary bottleneck equipment
- Quantify the Six Big Losses and identify your highest-leverage improvement priorities
- Deploy pragmatic solutions (SMED, TPM, Visual Controls) tailored to current resources
- Track daily trends, empower frontline operators, and sustain continuous Kaizen
Looking to Establish an OEE Measurement & Improvement System?
The INVAMAX expert team is ready to partner with your factory!
- Tailored Implementation Advisory
- Tailored to your specific factory realities
- Hands-on co-measurement and shopfloor improvement
- Delivering measurable, sustainable asset productivity